Hey there! I’m a supplier of home appliance stamping parts, and today I wanna chat about how to optimize the stamping process parameters of these parts. It’s a topic that’s super important for us in the industry, as it can directly impact the quality, efficiency, and cost of production. Home Appliance Stamping Parts
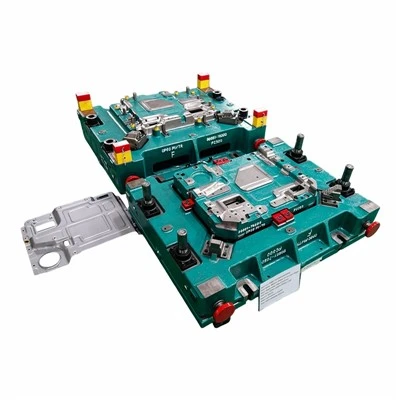
Let’s start by understanding the basics. The stamping process involves using a press and a die to shape metal sheets into the desired parts. The process parameters, such as the die clearance, punch speed, and blank holding force, play a crucial role in determining the outcome of the stamping process. If these parameters aren’t set correctly, we can end up with parts that have defects like cracks, wrinkles, or uneven thickness.
So, how do we optimize these parameters? Well, the first step is to have a good understanding of the material we’re working with. Different metals have different properties, such as hardness, ductility, and strength, and these properties can affect how the material behaves during the stamping process. For example, a softer metal like aluminum may require a different set of parameters than a harder metal like steel.
Once we know the material, we can start experimenting with different process parameters. This is where trial and error come in. We can start by making small adjustments to one parameter at a time and then testing the parts to see how they turn out. This can be a time – consuming process, but it’s the best way to find the optimal settings.
Let’s talk about die clearance. This is the space between the punch and the die. A proper die clearance is crucial for preventing burrs and ensuring the correct shape of the part. If the clearance is too small, the material may get stuck between the punch and the die, causing cracks or even damage to the die. On the other hand, if the clearance is too large, the part may have a rough edge or a distorted shape.
To find the right die clearance, we usually start with the recommended values based on the material type and thickness. Then, we make some test runs and adjust the clearance as needed. We look at the edges of the stamped parts to see if there are any signs of burrs or rough edges. If there are, we’ll decrease the clearance slightly and try again. If the parts seem to be getting stuck, we’ll increase the clearance.
Another important parameter is the punch speed. The speed at which the punch moves can affect the quality of the stamped parts as well as the efficiency of the production process. A higher punch speed can increase the production rate, but it may also increase the likelihood of defects. At high speeds, the material may not have enough time to deform properly, leading to cracks or wrinkles.
To optimize the punch speed, we need to consider the material properties and the complexity of the part. For thinner and more ductile materials, we can usually use a higher punch speed. But for thicker or less ductile materials, we may need to slow down the punch to ensure a good – quality part. We also need to make sure that the press can handle the chosen speed without any issues, so we’ll check the press capacity and performance.
Blank holding force is also a key factor. This force is used to hold the metal sheet in place during the stamping process to prevent wrinkling. If the blank holding force is too low, the material may wrinkle as it’s being formed. If it’s too high, it can cause excessive thinning of the material or even fracture.
We usually start with a standard blank holding force based on the material and part design. Then, we make some trial runs and observe the parts. If we see wrinkles, we’ll increase the blank holding force. If the parts are showing signs of excessive thinning or fracture, we’ll decrease the force.
In addition to these basic parameters, we also need to pay attention to the lubrication of the die and the metal sheet. Lubrication can reduce friction between the die and the material, which helps to prevent wear and tear on the die and improve the surface finish of the parts. There are different types of lubricants available, and we need to choose the one that’s suitable for the material and the stamping process.
We can also use some advanced techniques to optimize the stamping process parameters. One of these is finite element analysis (FEA). FEA is a computer – based simulation method that can help us predict how the material will behave during the stamping process. By using FEA, we can test different process parameters and part designs without having to make physical prototypes. This can save a lot of time and money in the long run.
Another technique is statistical process control (SPC). SPC involves collecting data on the stamping process and using statistical methods to analyze the data. This can help us identify trends and variations in the process, and take corrective actions before any major defects occur.
Now, as a home appliance stamping parts supplier, I know that optimizing the stamping process parameters is not only about improving the product quality but also about meeting the customer’s needs. Customers are always looking for high – quality parts at a reasonable price, and by optimizing our process parameters, we can achieve both.
We can offer better – quality parts because the optimized parameters will reduce the number of defects, ensuring that the parts meet the strict quality standards. At the same time, we can lower our production costs by improving the efficiency of the process. This means we can pass on some of the savings to our customers, making our parts more competitive in the market.
If you’re in the home appliance industry and are looking for a reliable stamping parts supplier, I’d love to talk to you. I can share more about how we optimize our stamping process parameters and how we can meet your specific requirements. Whether you need small – scale or large – scale production, we have the expertise and the resources to deliver high – quality parts on time.
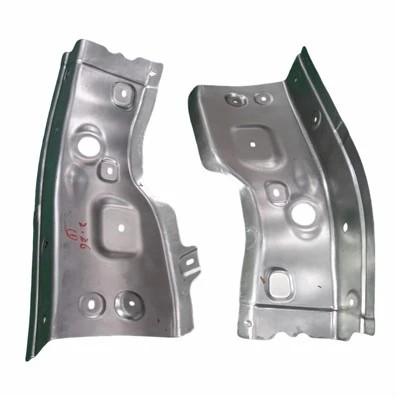
So, if you’re interested in discussing your stamping parts needs, don’t hesitate to reach out. We’re always happy to have a chat and see how we can work together to create the best home appliance stamping parts for your products.
Home Appliance Stamping Parts References:
- "Metal Stamping Handbook" by American Iron and Steel Institute
- "Sheet Metal Forming Processes and Die Design" by Kalpakjian, S.
Dongguan Changdong Tool & Die Co., Ltd.
With abundant experience, we are one of the most reliable home appliance stamping parts manufacturers and suppliers in China. Please feel free to buy advanced home appliance stamping parts made in China here from our factory. Good service and quality products are available.
Address: No. 56-B, Fumin South Road, Dalang Town, Dongguan City, Guangdong Province, China
E-mail: sales@stamping-die.com
WebSite: https://www.metalstampingdie.com/
