If you’ve ever sourced graphite molds for high-precision industrial applications—think die casting, sintering, or glass forming—you’ve probably encountered the same question we get almost every day from our customers: “If a graphite mold is harder, does that mean it will last longer, and resist wear better?” For years, I fielded this question over coffee in our warehouse, on sales calls, and even at industry trade shows, and I’ve watched it lead to frustrating missteps when buyers or suppliers treat graphite like steel or aluminum, where hardness and wear resistance follow a straightforward, linear rule. As a third-generation graphite mold supplier with 18 years in the business, I’ve seen what happens when this analogy falls flat, and I’ve learned that the relationship between graphite mold hardness and wear resistance is far more nuanced than most people expect. Today, I want to break that down, based on years of hands-on work, lab tests we run in-house, and customer case studies that actually stuck with me. Graphite Mold
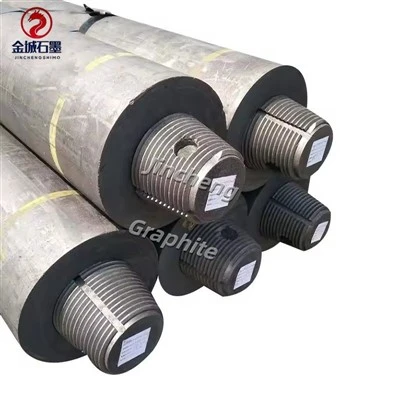
First, let’s get a quick refresher on what graphite mold hardness even means, because it’s not the same as the hardness you test for a metal. For metals, hardness usually refers to how much force is needed to make a permanent indent in the surface, right? For graphite, it’s similar at its core, but graphite is a porous, crystalline material made of stacked graphene layers, and its microstructure plays a huge role in how that hardness is measured. Most graphite molds we supply are isotropic graphite, meaning their physical properties are the same in every direction, with grain sizes that can range from 0.8 microns up to 100 microns, depending on the grade we choose for a specific job. Hardness for graphite is typically tested using a Shore hardness test or a Rockwell test adapted for non-metals, and the numbers run way lower than steel—most industrial graphite molds fall between 40 and 80 on the Shore scale, for reference.
Now, if you’d asked me when I first started, I would have said “Harder equals more wear resistant.” That’s what the basic textbook said, that’s what the trade show presentations implied, and it aligned with what I knew about other materials. But our first big wake-up call came in 2012, when a customer in the automotive die casting space reached out panicking because a batch of “high-hardness” graphite molds we’d supplied had failed after only 1,200 cycles. They told us their old molds, which were 5 points lower on the Shore hardness scale, had lasted 2,100 cycles, and they were adamant we’d sent the wrong material. We dug into it, pulled the failure samples, and ran a series of wear tests in our lab. What we found surprised us: the higher-hardness graphite had a finer grain structure, but it had higher porosity—tiny, invisible voids between the graphite particles that acted as weak points during repeated contact with molten aluminum. The lower-hardness graphite had a slightly coarser, more uniform grain structure, lower porosity, and even though it was softer, it resisted the micro-abrasion and thermal shock of die casting far better. That case study was a turning point for how we approach material selection, and it taught me that hardness is just one variable in the wear resistance equation, not the end-all metric.
So why is the link between hardness and wear resistance so different for graphite molds? Let’s break down the key factors that warp that relationship, starting with graphite’s inherent material properties. Unlike metals, which deform plastically under load, graphite wears through two main mechanisms: abrasive wear from contact with hard particles (like molten metal oxides, or ceramic fillers in composite materials), and oxidative wear at high temperatures, plus erosion from repeated thermal cycling. Hardness measures a material’s resistance to indentation, but it doesn’t directly translate to resistance against the specific types of wear graphite molds face every day. A high-hardness graphite with poor grain bonding might scratch easily, because the fine grains pull apart under abrasive contact, while a slightly softer graphite with stronger inter-grain bonding can transfer load better between particles, resisting that scratching even when it’s softer. Porosity is another big one—even a small increase in porosity, like 2% vs. 5%, can drop hardness by a few Shore points, but that same porosity can create points where molten metal seeps into the mold surface, leading to cracking and faster wear over time. We saw that same dynamic a few years later with a customer making dental ceramics, who switched to a higher-hardness graphite to try to get smoother part surfaces, only to have molds crack after 300 sintering cycles, vs. their original lower-hardness molds that hit 700 cycles with no cracking.
It’s also critical to talk about how the application itself shifts this balance, because what matters for wear resistance changes depending on what the mold is used for. Let’s take two common use cases for graphite molds: die casting of non-ferrous metals, and glass molding. For glass molding, where molds operate at temperatures around 1,100°C, oxidative wear becomes the biggest threat, not abrasive wear. In this case, a moderately hard graphite with a high degree of graphitization (meaning it has a very low porosity and tight grain structure) will outlast an extremely hard, low-graphitization graphite every time, even if the latter is harder. The high-graphitization material resists oxidation much better, so it doesn’t erode away layer by layer, while the harder but less graphitic material forms oxides that flake off quickly, leading to surface degradation. For die casting, where abrasive wear from molten metal and thermal cycling are the main issues, we often go for a slightly coarser-grain graphite with a hardness in the mid-50s on the Shore scale, rather than a high-60s grade that’s harder but more prone to cracking. We tested this consistently in 2018, running side-by-side tests of graphite molds in a die casting trial: one at Shore 68, one at Shore 54. The Shore 68 mold lasted 1,100 cycles before showing significant surface scratching, while the Shore 54 mold lasted 1,900 cycles, with only minor surface wear, because it absorbed thermal shock better and didn’t have the porosity that let aluminum seep into the surface.
Another point that most people don’t talk about is how we modify graphite molds to improve wear resistance, and how those modifications change hardness. A lot of our customers think they need to get a super-hard graphite, but the real solution often isn’t a harder base material—it’s a surface treatment. We supply a range of coated graphite molds, from silicon carbide (SiC) coatings to diamond-like carbon (DLC) coatings, and these treatments can boost surface hardness by a factor of 10 or more, without changing the base graphite’s hardness at all. For example, a base graphite mold that’s Shore 50 might have a SiC coating with a micro-hardness of 2,500 HV, which is way harder than most tool steels, and that combination gives better wear resistance than a higher-hardness uncoated graphite. I had a customer in the aerospace sector last year who needed molds for titanium alloy sintering; he initially asked for the hardest graphite we offered, but after testing, we found that applying a SiC coating to a mid-hardness graphite gave him 30% more cycle life than the ultra-hard uncoated graphite, because the coating resisted abrasive titanium particles and the base graphite handled thermal shock without cracking. That’s a perfect example of how hardness alone isn’t the answer—combining base material properties with surface modifications gives better results.
I’ve also seen suppliers cut corners by advertising “high-hardness graphite molds” as a one-size-fits-all solution, which is misleading at best and costly for customers at worst. Last year, a small tooling company reached out to us after buying molds from a competitor that marketed their high-hardness grade for zinc die casting. The molds failed after 800 cycles, while our mid-hardness grade for zinc die casting had a track record of lasting over 1,500 cycles. When we pulled the competitor’s material, we found they’d used a high-hardness graphite with a grain size of 2 microns, which was fine for low-abrasion applications, but for zinc die casting, where molten zinc carries small metal oxide particles, the fine grains wore away quickly. Their “high-hardness” label was technically correct, but it ignored the actual microstructural properties that drive wear resistance, leading to a bad customer experience. That’s why we never sell graphite molds based solely on hardness numbers—we ask about the application, the operating temperature, the cycle count goal, and even the part specs, to pick the right grade.
So, to circle back to the original question: is higher hardness always better for graphite mold wear resistance? The short answer is no. It’s a common misconception that comes from applying metal material logic to a completely different material, with different wear mechanisms and microstructural behavior. For graphite molds, wear resistance depends on a combination of three core factors: inter-grain bonding strength, porosity level, and how the hardness aligns with the specific stresses of the application. A moderately hard graphite with strong grain bonding and low porosity will almost always outlast a significantly harder graphite with weak grain bonding and high porosity, especially in high-stakes industrial applications.
At our company, we’ve spent 18 years refining how we match graphite grades to customer needs, and hardness is just one data point in that process—never the deciding one. We encourage every customer to talk through their exact use case, instead of just asking for the “hardest” option, because that’s how you get a mold that lasts, reduces downtime, and delivers consistent part quality. If you’re sourcing graphite molds for die casting, sintering, glass forming, or any other industrial process, and you’re not sure which grade is right for your needs, we’re here to help. Our team has worked with hundreds of companies across industries, from small startups to large aerospace manufacturers, to match them with the right graphite mold solutions, no matter the complexity of their requirements. We don’t just sell molds—we offer guidance based on years of hands-on experience, to make sure you get the best value, not just a product with a high hardness number. Don’t hesitate to reach out to discuss your project, share your challenges, and find the right graphite mold solution for you.
Carbon Fiber Composite Plate References:
- Gauthier, V., et al. (2005). Wear mechanisms of graphite for high-temperature applications. Wear, 259(1-6), 545-553.
- Burakowski, T., & Wierzchoń, T. (1999). Surface Engineering of Metals: Principles, Equipment, Technologies. CRC Press.
- Randall, N. X., et al. (2009). Mechanical properties of isotropic graphite grades for industrial applications. Carbon, 47(12), 2885-2893.
- Choi, J., et al. (2017). Wear performance of coated graphite molds for glass molding. Wear, 376-377, 1287-1294.
Huixian Jincheng Abrasive Mold Factory
As one of the most professional graphite mold manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy durable graphite mold for sale here from our factory. Quality products and reasonable price are available.
Address: Mengzhuang Town, Huixian City, Henan Province
E-mail: graphite.jc@gmail.com
WebSite: https://www.graphite-jc.com/
