If you work in manufacturing, especially as a complex parts supplier like me, you know that getting accurate dimensions isn’t just a box to tick—it’s the whole reason clients come back. I’ve seen too many shops cut corners on measurement, only to get a $10k rework bill or a lost contract. Over the 12 years I’ve run my shop, we’ve tested every trick in the book for tricky parts—think aerospace turbine blades with twisted airfoils, medical implant housings with internal undercuts, or automotive gear assemblies that blend precision and tight tolerances. Today, I’m breaking down what actually works, no fancy jargon, just the stuff we’ve put to use on hundreds of jobs. Complex Parts
First, let’s get one thing straight: a “complex part” isn’t just a weird shape. It’s any part that has features you can’t measure with a standard caliper or tape. That might mean hidden internal cavities, curved surfaces, tight tolerances (like +/- 0.0005 inches) that are smaller than a human hair, or multiple intersecting angles that throw off basic tools. For us, 80% of the parts we make fall into this category, so we’ve built our process around avoiding the mistakes most people make with simple tools.
The biggest mistake I see? Relying on a single measurement tool. A lot of new guys will grab a digital caliper, snap it across a part, and call it good. But calipers only measure linear distances—if your part has a contoured surface, or a hole with a sloped wall, that caliper reading is useless. Last year, a client sent us a batch of small titanium brackets that their in-house team had measured with calipers, thinking the inner pocket was 0.250 inches deep. Turns out, the pocket had a 15-degree taper, so the actual depth at the deepest point was 0.262 inches—enough to make the bracket not fit their assembly. We had to rework 120 pieces, and they almost took their business elsewhere. Lesson learned: match your tool to your feature, not the other way around.
So, let’s talk about the tools we actually use, and when to use each.
First up, coordinate measuring machines (CMMs). These are workhorses for complex parts, especially high-volume or precision jobs. A CMM uses a probe that moves across the part’s surface, collecting thousands of data points to build a 3D digital model. We use three types here: touch-trigger CMMs, scanning CMMs, and portable CMMs, depending on the part. Touch-trigger is for simple, defined features—holes, bosses, flat surfaces. Scanning CMMs are the real deal for contoured parts, like turbine blades or orthopedic implants. They glide the probe along curves, so you don’t miss the subtle twists that calipers would skip. Portable CMMs are game-changers for large parts, like automotive chassis brackets that can’t fit inside a fixed CMM. We wheel our portable arm right to the shop floor, hook it up to the part, and get accurate readings without moving the part. The key here is calibrating the CMM every single day—no exceptions. A 0.001-inch miscalibration will throw every measurement off, and we’ve skipped calibration once (on a super tight deadline) and had to scrap a whole run of parts. Never do that.
Next, optical measurement systems, like video comparators or laser scanners. These are perfect for parts with tiny features, especially delicate stuff where a physical probe could scratch the surface. For example, we make small plastic components for insulin pumps that have micro-features (some less than 0.005 inches wide) that would break if a probe touched them. A video comparator shines light on the part, captures a high-res image, and lets you measure features pixel by pixel—way more accurate than a manual tool. Laser scanners take this even further: they fire thousands of laser points per second to create a 3D point cloud of the part, which you can compare directly to your CAD model to spot deviations. We use laser scanners for parts with super tight tolerances, like fuel injector nozzles, because they can pick up tiny gaps or uneven curves that a CMM might miss. One tip here: if you’re using optical tools, make sure the part is clean and free of debris. A single dust particle can look like a 0.01-inch feature, and you’ll waste hours chasing a “defect” that doesn’t exist.
Then there’s the old-school stuff that still works: micrometers, height gauges, and pin gauges, but only if you use them right. Micrometers aren’t for everyone, but they’re great for basic linear measurements on parts that are too big for calipers. Height gauges, with a digital readout, work for measuring the height of features like bosses or steps on a part, but you have to make sure the part is sitting perfectly flat on a granite surface plate. Pin gauges are essential for measuring hole diameters, especially small or threaded holes—just make sure you test multiple pins to get the right fit, not just one. We still keep a full set of precision pin gauges on the floor, because sometimes a small hole is easier to check with a pin than a CMM, and it’s way faster for quick inspections.
Now, even with the right tools, you have to set up the part correctly, or your measurements will be garbage. This is where a lot of shops slip up. You can’t just plop a part on a table and start measuring—you need to secure it properly and align it to your CAD model, not just the part’s rough edges. For example, a complex part might have a rough cast surface, so if you align your CMM to those edges, all your measurements will be off by a few thousandths of an inch. Instead, we use datum features—reference points or surfaces that are machined to exact specs— to align the part. Last month, we had a set of engine manifolds that had a few rough casting edges. By aligning the CMM to the two precision bolt holes (our datums) instead of the outer edge, we got measurements that were within +/- 0.0003 inches, which is exactly what the client needed. Another big tip: always measure multiple features, not just one. If a part has two holes, measure both to make sure their spacing is correct, not just their individual diameters. A single off hole might pass inspection, but two could break the whole assembly.
We also run a secondary check on every part, no exceptions. Even if the CMM says it’s good, we’ll pull it off the fixture and measure a key feature with a different tool to confirm. For example, if a CMM scans a turbine blade’s airfoil, we’ll snap a quick measurement with a laser micrometer on the blade’s leading edge to make sure the CMM reading wasn’t skewed by a probe calibration error. One time, we had a CMM give us a perfect reading, but when we checked with a laser scanner, we found a tiny 0.0004-inch deviation that the CMM had missed. If we’d only gone with the CMM, those parts would have been rejected at the client’s facility, costing us time and our reputation. Secondary checks aren’t a waste of time—they’re the difference between a reliable supplier and one that makes mistakes.
Let’s talk about specific examples, because that’s where this stuff matters most. Last quarter, we made a batch of 500 orthopedic hip stems for a medical device client. These parts have a tapered neck that mates with a femoral head implant, and the tolerance on that taper was +/- 0.001 inches—super tight, and if it’s off, the implant won’t seat right, which could cause pain or surgery revisions. We used a scanning CMM to map the entire taper, but we also used a coordinate measurement arm to check the neck’s angle manually. We caught two parts where the taper was off by 0.0012 inches—barely enough to miss, but we pulled them and reworked them. The client didn’t even ask for a secondary check, but we did it because that’s how we operate. Another example: we make aerospace wing ribs that have multiple intersecting angles. Using a basic caliper to measure the angle would give us a rough number, but we use a rotary table on a CMM to set the part’s rotation exactly, then measure the angle to within 0.05 degrees. That’s the stuff that keeps planes in the sky.
Now, what about common pitfalls to avoid? First, don’t skip tool calibration. We calibrate all our tools—CMM, laser scanner, micrometers—daily, before we start any job. If a tool is off, you can’t trust any reading. Second, don’t rush measurements. It’s tempting to blast through a job when you’re on a deadline, but taking 10 extra minutes to set up the part correctly and get multiple readings will save you hours of rework later. Third, don’t ignore your CAD model. Your CAD file is the blueprint, so always align your measurements to that, not just the physical part. Parts can have casting or machining variation, so comparing your measurements to the CAD model’s target is the only way to get accuracy. Fourth, don’t use the wrong tool for the job. If you’re measuring a tiny delicate part, don’t use a touch probe—it’ll scratch or break it. Use optical instead. If you’re measuring a large part, don’t drag a small portable CMM—use a larger arm or laser tracker.
For our shop, all this has paid off. We’ve maintained a 98% on-time delivery rate, and our repeat business is over 85% because our clients know our parts fit every single time. We’ve had clients come to us from other suppliers because their parts were getting rejected at their inspection, and we fixed the measurement errors on their first batch. It’s not magic—it’s just sticking to a consistent process, using the right tools for the job, and double-checking everything.
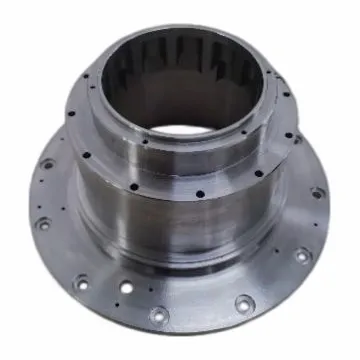
If you’re a procurement manager or engineer dealing with complex parts, here’s what I want you to take away: accurate measurement isn’t about the fanciest tool—it’s about matching the tool to the feature, setting up the part right, and verifying your results. If you’re tired of dealing with parts that don’t fit, or rework that kills your timeline, get in touch. We work with all kinds of industries—aerospace, medical, automotive—and we can help you get the accurate parts you need, on time, every time.
MWIR Thermal Imager 640 References
- ASME B89.4.22-2004, Methods for Performance Evaluation of Coordinate Measuring Machines (CMMs)
- De Chiffre, L., et al. (2003). Industrial Applications of Optical Measurement Techniques for Precision Parts. CIRP Annals – Manufacturing Technology, 52(2), 551-574.
- Smith, G. S. (2010). Metrology and Properties of Engineering Surfaces. Springer Press.
- Aerospace Industries Association (AIA) Standard AIA-NQA-10, Non-Destructive Testing and Measurement Requirements for Aerospace Components
Xi’an Zhongke Lead Ir-Tech Co., Ltd.
We are one of the most experienced complex parts manufacturers in China, specialized in providing high quality OEM products with the industrial grade. We warmly welcome you to wholesale high performance complex parts at an affordable price from our factory.
Address: Building 8,Hard Technology Enterprise Community No.3000,Biyuan 2nd Rd,High-Tech Zone Xi’an,Shaanxi,China
E-mail: sales@lead-ir.com
WebSite: https://www.leadinfrared.com/
